Most folding machine purchases go wrong in the same way: the buyer specifies the largest sheet they might one day run and the fastest speed in the brochure, and then discovers that the machine cannot control the miniature leaflet that pays the bills. Specifying in the right order avoids this, because each decision removes machines from the list and the remaining choices get easier.
Below is the order we use with customers. Bring these seven answers to any supplier and the conversation becomes a specification exercise rather than a sales pitch.
Step 1 · The smallest sheet, not the largest
Start with the smallest finished job in your order book, not the biggest sheet in your warehouse. A machine is limited at both ends, and the small end is where control is lost: 60 × 100 mm is the floor on the T490 platform, 150 × 150 mm on the T780.
Note · If you fold pharmaceutical leaflets and commercial brochures, the leaflet size decides the platform, and the brochure size decides whether you also need a second machine.
Step 2 · Paper weight range
Paper weight sets the roller pressure, the creasing setting and often the feeder type. The small-format buckle platforms run 28–200 gsm; the T780 runs 40–210 gsm. If your work includes cover stock above the range, plan for creasing before folding or a knife fold for the difficult panels.
Step 3 · List the fold patterns you quote
Write down the patterns, not the product names: half fold, tri-fold (letter), gate fold, accordion (concertina), double parallel, cross fold, and how many panels each has. This list is what determines the plate configuration, and it is far more useful to a supplier than "brochures".
- Simple parallel and letter folds are reachable from a small plate set.
- Multi-panel accordion and gate folds need correspondingly more plates.
- Heavy cross folds benefit from an extended-delivery plate variant that keeps grip on the last pass.
- Right-angle folds on cover stock are often cleaner on a knife or on a combination machine.
Step 4 · Plate count and configuration
Plate count is the single most under-specified number in folding machine enquiries. One machine makes one fold per pass, so the plate set determines which patterns are reachable without re-threading. A 10+4 set covers most direct-mail and brochure work; 12+6 and 14+6 reach further; the choice should be driven by the pattern list from step 3.
Step 5 · Feeder and pile height
The feeder decides who operates the machine. A standard automatic feeder with suction-wheel separation is enough for intermittent work. For continuous production, a round-pile or recirculating feeder on the T600/T780 platform lets the pile be rebuilt while folding continues — which is what makes one-operator, two-machine layouts realistic.
Step 6 · Speed you will actually run
Rated speed (180 m/min on the T490/T520/T600 platform, 210 m/min on the T780) is a ceiling, not a working speed. The real question is the fastest speed at which your stock folds within tolerance, and that is a question about paper, plate settings and grip. A supplier who will not run your paper before quoting a speed is guessing.
Step 7 · Delivery, footprint and services
Finally, the constraints that decide whether the machine can be installed at all: delivery type (belt or vertical stacker), machine dimensions and weight, power supply and air supply.
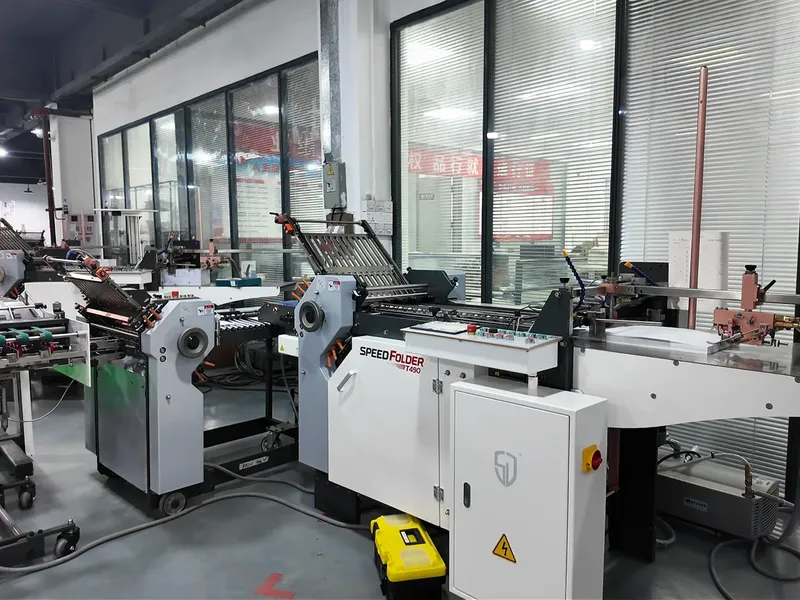
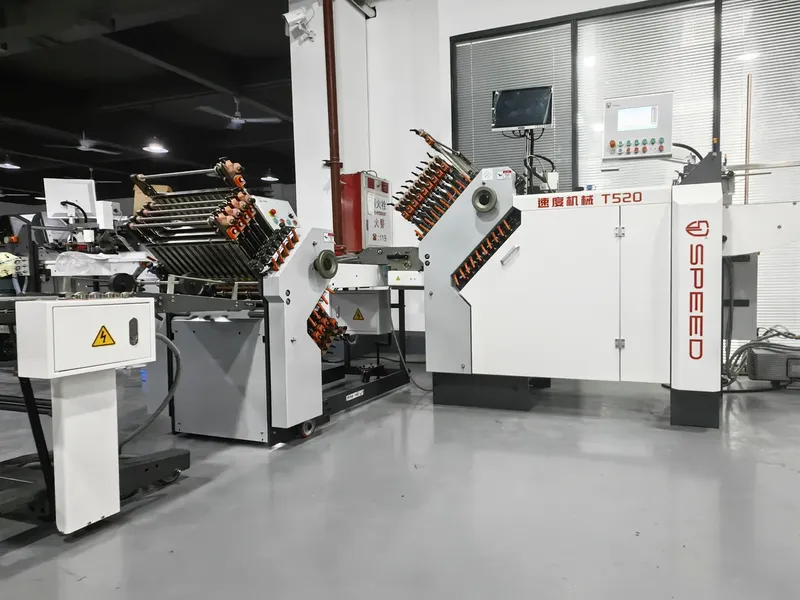
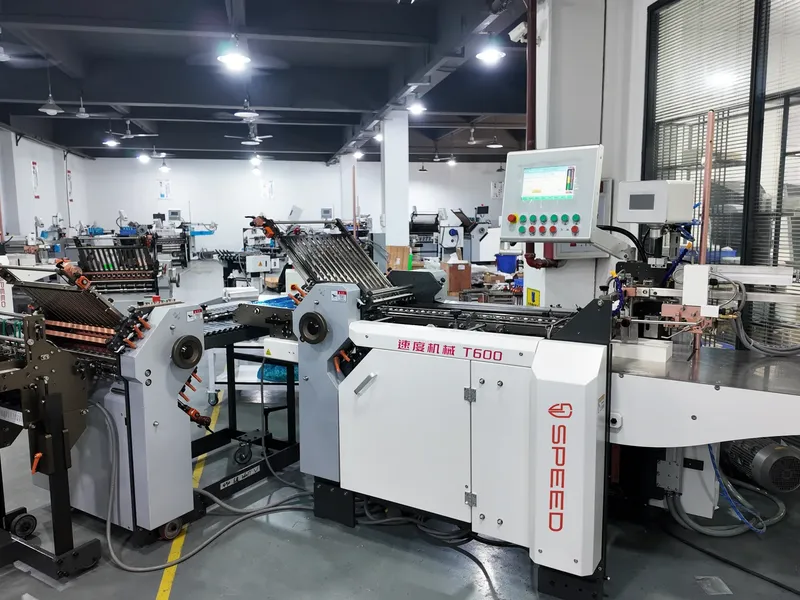
- T490/T520/T600 platform: 4650 × 1100–1200 × 1500 mm, 990–1200 kg, 3.5 kW, 380 V.
- T780: 4300 × 1700 × 3500 mm, 1560 kg, 5 kW, 380 V.
- SD-X250 knife unit: 1250 × 752 mm, 0.9 kW, 220 V, 0.4–0.6 MPa air.
What to send a supplier
The fastest route to a correct quotation is a single message containing these six items.
- Unfolded sheet size and paper weight in gsm
- Finished folded size, and the panel layout if it is not a standard pattern
- Monthly or weekly quantity
- Whether folding is standalone or inline with stitching, gluing or cartoning
- Any tolerance or qualification requirement (pharmaceutical documentation, customer spec)
- Available floor space, power supply and air supply
Note · With those six answers we fold a sample on your stock and return it with measurements, so the decision is made on a physical result rather than a datasheet.
Frequently asked
Should I buy the largest machine I can afford?
How many buckle plates should I specify?
Do I need a knife folder as well as a buckle folder?
How do I verify fold quality before ordering?
Related footage
Instruction-manual folding with a vertical stacker
Miniature instruction-manual folding with the vertical stacker module — the configuration pharmaceutical printers use to keep small panels aligned at the delivery.
Watch on YouTube →Instruction-manual folder on the factory floor
Build and assembly detail of a miniature instruction-manual folder — folding fences, sealed lubrication box and gear transmission.
Watch on YouTube →